- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
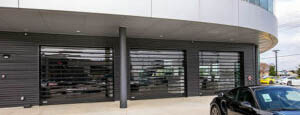
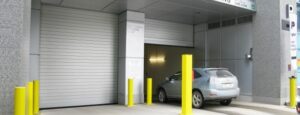
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
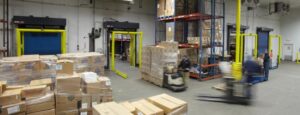
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
China Top Mechanical Seal for Water Pump Suppliers?
Choosing a reliable China supplier for a Mechanical Seal For Water Pump requires more than comparing prices. Water quality, pump speed, temperature, pressure, and shaft size all affect seal performance. A supplier experienced with municipal systems may not suit chemical processing equipment. This difference matters.
A strong manufacturer should provide material options, including ceramic, silicon carbide, carbon, stainless steel, and elastomers. Each selection should match the fluid and operating conditions. Product drawings, tolerance data, testing records, and installation guidance can reveal genuine technical capability. Ask whether the factory performs pressure testing and dimensional inspection before shipment. Small details often prevent large failures.
Look for suppliers with stable production, traceable components, and responsive engineering support. Factory audits, sample orders, and customer references offer practical evidence. Certifications may help, but certificates alone do not prove consistent quality. That assumption needs examination. A polished website is not enough.
Real-world experience also matters. A seal running continuously beside a hot pump casing faces different stress from one used in a cool water tank. Packaging should protect polished faces from dust, impact, and moisture during transport. Clear communication about drawings and tolerances reduces costly misunderstandings.
This guide examines leading Chinese suppliers through product quality, customization, delivery reliability, technical service, and after-sales support. It also considers where supplier claims may require verification. No manufacturer fits every application. Careful selection remains essential. Even a minor mismatch can cause leakage, vibration, downtime, and premature replacement.
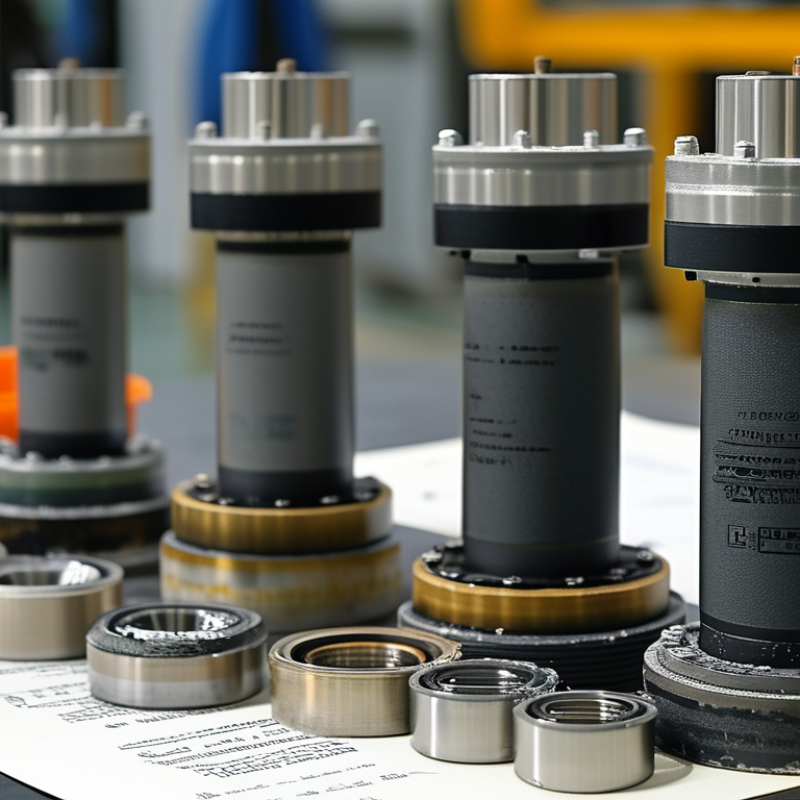
Table of Contents [Hide]
What Is a Mechanical Seal for a Water Pump?
What Is a Mechanical Seal for a Water Pump?
A mechanical seal prevents water from escaping where the rotating shaft leaves the pump casing. It uses two finely finished faces, usually carbon and ceramic or silicon carbide. A spring pushes these faces together. A thin water film reduces friction and heat. The seal also contains elastomers, a spring, and secondary sealing parts.
Selection depends on more than pump size. Water temperature, pressure, shaft speed, suspended particles, and chemical treatment all matter. Clean water may suit carbon and ceramic faces. Abrasive water often needs harder materials. Incorrect alignment can create a narrow leakage line around the shaft. A small mistake matters.
The U.S. Department of Energy’s Improving Pumping System Performance sourcebook reports that pumping systems may represent 25% to 50% of industrial facility electricity use. A leaking seal can waste water and increase maintenance, although the seal itself is rarely the largest energy loss. ANSI/HI 9.6.3 guidance also stresses operating pumps near their preferred range, which helps reduce vibration and seal wear. In field inspections, checking dry running, shaft runout, and installation damage is essential. The choice is not always elegant. A lower-cost seal may perform well in clean water, but fail quickly under heat, grit, or frequent starts. Reliable suppliers should provide material certificates, dimensional drawings, pressure limits, and test records.