- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
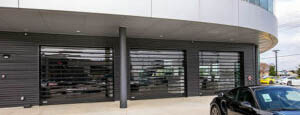
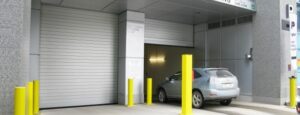
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
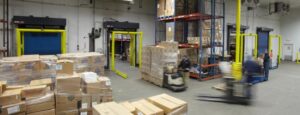
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
China Best Stainless Threaded Rod Supplier?
Choosing the China Best Stainless Threaded Rod Supplier? The answer depends on more than price, product photos, or a polished website. Buyers need consistent threads, accurate dimensions, reliable material grades, and stable delivery. Stainless Threaded Rod products may look similar on a screen. Their performance can differ greatly on a construction site or inside a production line.
This guide examines how experienced buyers evaluate Chinese manufacturers and exporters. It considers common grades, including 304 and 316 stainless steel, along with metric and imperial thread options. Details matter. A practical inspection should check thread smoothness, rod straightness, surface finish, and actual diameter. Samples can be measured with thread gauges before larger orders are approved. Mill certificates and inspection reports also help confirm material claims. They are useful, not magical.
Supplier experience should be visible in technical communication, production records, packaging methods, and responses to difficult questions. A dependable company can explain tolerances, cutting services, heat treatment, minimum order quantities, and lead times clearly. It should also identify limitations instead of promising everything. No supplier is perfect. Some factories may offer excellent machining but weaker export support. Others may provide fast communication but limited quality documentation.
For corrosion-sensitive applications, buyers should match the stainless grade to the environment, load, and installation conditions. Coastal air, chemical exposure, and trapped moisture can change the decision. This article will compare manufacturing capability, quality control, customization, pricing, and after-sales support. The goal is not to promote the cheapest option. It is to help readers select a reliable China-based partner with evidence, practical judgment, and fewer costly surprises.
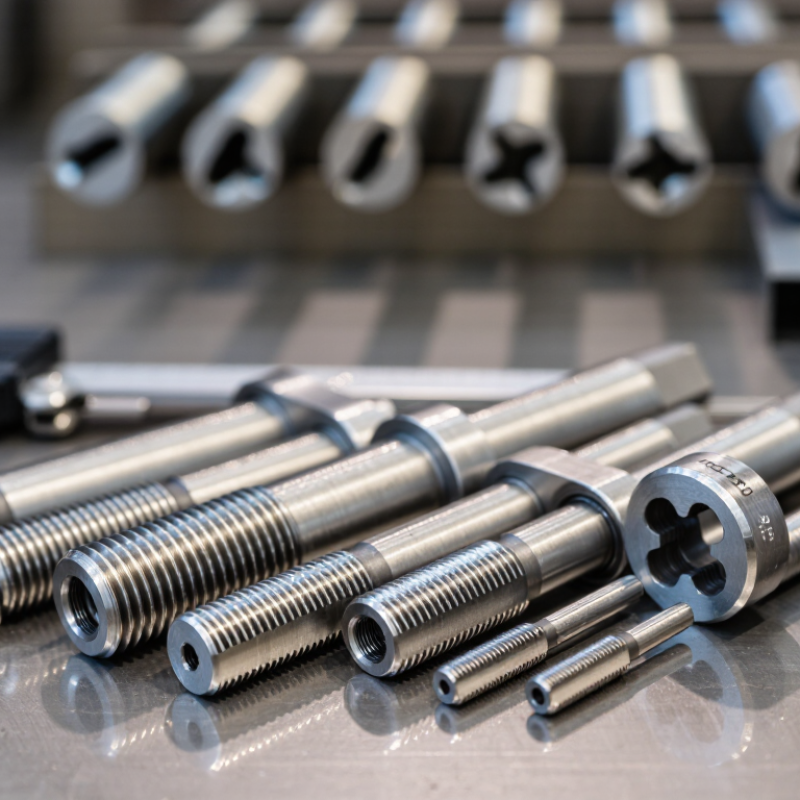
Table of Contents [Hide]
Stainless Threaded Rod Grades: 304, 316, and 316L with 16–18% Chromium
Choosing the best stainless threaded rod supplier in China starts with grade control, not appearance. Grade 304 commonly contains about 18–20% chromium, while 316 and 316L usually contain 16–18% chromium. These ranges follow chemistry requirements referenced in ASTM F593 and ISO 3506-1. Chromium forms a passive oxide layer, helping rods resist moisture and surface corrosion.
Grade 304 suits indoor frames, machinery, and general construction. Grade 316 adds molybdenum, normally around 2–3%, improving resistance to chlorides and coastal exposure. Grade 316L keeps similar chromium and molybdenum levels, but its carbon limit is lower, typically 0.03% maximum. That detail reduces carbide precipitation after welding. It matters in fabricated assemblies.
Small differences matter.
The International Stainless Steel Forum reported global stainless crude steel production of approximately 58.4 million tonnes in 2023. This figure shows the scale of demand, but it does not guarantee threaded rod quality. In practical purchasing, I check heat numbers, mill certificates, thread gauges, and salt-spray or corrosion-test records. A common mistake is choosing 316 solely because it sounds stronger. It is usually more corrosion-resistant, not automatically stronger. Thread fit, tensile class, surface finish, and traceability still require verification. Some suppliers provide attractive certificates, yet inspection may reveal mixed batches or incomplete chemical data. That is where careful sampling becomes necessary.