- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
China Best Rod Breakdown Machine Supplier?
Finding the China Best Rod Breakdown Machine Supplier requires more than comparing prices or polished factory photos. It requires practical evidence from copper and aluminum wire production. A dependable supplier should explain drawing speed, rod diameter ranges, die-box design, cooling methods, electrical controls, and finished-wire accuracy. These details directly affect surface quality, energy use, and maintenance intervals.
Wire-processing consultant David R. Hughes states, “A rod breakdown machine earns trust through stable output, not impressive specifications.” His point matters on the factory floor. A machine may advertise high speed, yet vibration can create uneven wire surfaces and frequent die replacement. Ask suppliers for test-run videos, sample data, component brands, and measured production results. Better still, request a trial using your own rod material.
Experienced manufacturers in China can offer customized layouts, automated tension control, and responsive technical support. However, “customized” does not always mean better. Extra functions may increase adjustment difficulty and spare-parts costs. That deserves careful reflection.
A credible Rod Breakdown Machine supplier should provide installation guidance, operator training, preventive-maintenance schedules, and clear warranty terms. Check whether engineers understand your target conductor size, alloy, output volume, and plant conditions. Look for documented inspection records, not only promises. Small details matter: clean cable routing, accessible lubrication points, guarded rotating parts, and stable temperature control.
The best choice is rarely the cheapest quotation. It is the supplier that combines repeatable performance, transparent communication, and practical after-sales service. Even a strong supplier can make mistakes. That is why factory audits, reference checks, and acceptance testing remain essential before purchase.
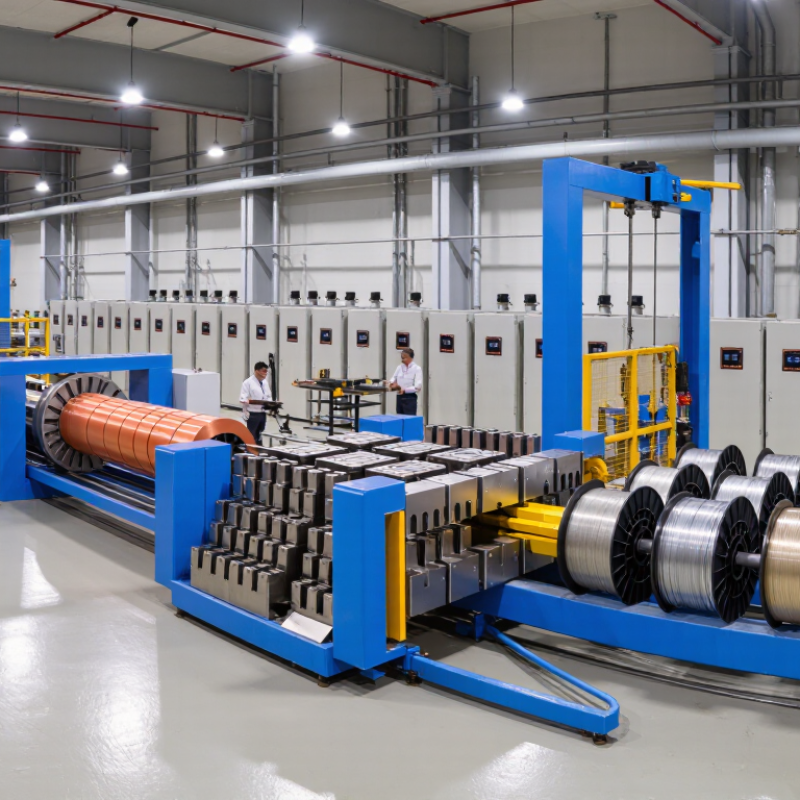
Table of Contents [Hide]
What Is a Rod Breakdown Machine?
A rod breakdown machine is industrial equipment that reduces the diameter of metal rod through repeated drawing. It prepares copper, aluminum, or other suitable wire materials for later production stages. The rod enters through a pay-off system and passes through hardened dies. Each die applies controlled pressure and reduces the cross-section gradually. Several drawing blocks work in sequence. The finished wire leaves thinner, longer, and more uniform. Small details matter. Lubrication limits friction and helps prevent surface scratches. Cooling systems remove heat created during high-speed drawing. Without stable tension, the rod may twist, break, or develop uneven dimensions.
When evaluating a rod breakdown machine supplier in China, request clear technical specifications and tested production data. Ask about maximum inlet diameter, outlet range, drawing speed, motor control, die compatibility, and cooling capacity. A reliable supplier should explain maintenance intervals and provide practical installation guidance. Check how the machine handles emergency stops, tension changes, and routine die replacement. These details reveal more than polished photographs. In plant trials, operators often notice vibration before instruments show a serious problem. That observation deserves attention. No machine performs perfectly under every material condition. Rod hardness, lubricant quality, and ambient temperature can change results. A thoughtful supplier discusses these limitations instead of promising effortless operation. Good engineering includes honest adjustment.