- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
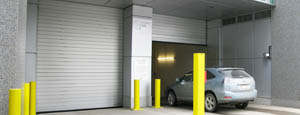
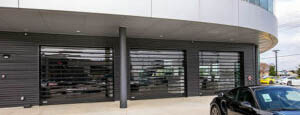
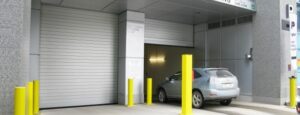
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
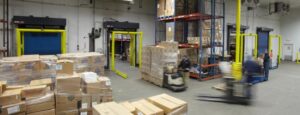
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
Best Lead Apron Manufacturer in China for Global Buyers
Choosing the best lead apron manufacturer in China requires more than comparing catalog prices. Global buyers need dependable protection, consistent quality, and clear communication. A trusted supplier should understand hospital workflows, dental imaging rooms, veterinary clinics, and mobile radiography teams. Each setting creates different demands for weight, flexibility, storage, and cleaning.
Dr. John W. Boice Jr., a respected radiation-protection expert and former NCRP president, emphasized the established principle of keeping exposure “as low as reasonably achievable.” This principle should guide every lead apron decision. Buyers should examine the apron’s lead-equivalent rating, protective coverage, stitching, closures, and internal shielding material. They should also request batch testing, inspection records, and practical wearing instructions. A strong manufacturer can explain these details without hiding behind vague technical language.
Small details matter. The shoulders should not feel overloaded after a long procedure. The front panels should overlap properly. Hooks and fasteners should remain secure after repeated use. Storage instructions should prevent sharp folds and avoid unnecessary damage. Yet no supplier is perfect. Samples may feel different from bulk production, and attractive product photos can conceal uncomfortable weight. Buyers must test representative samples and review quality controls before placing a large order. Honest factories should accept reasonable questions, document corrective actions, and improve when weaknesses appear. For global buyers, the best lead apron manufacturer is not simply the lowest-cost exporter. It is a responsive partner that combines measurable protection, careful production, transparent documentation, and practical experience.
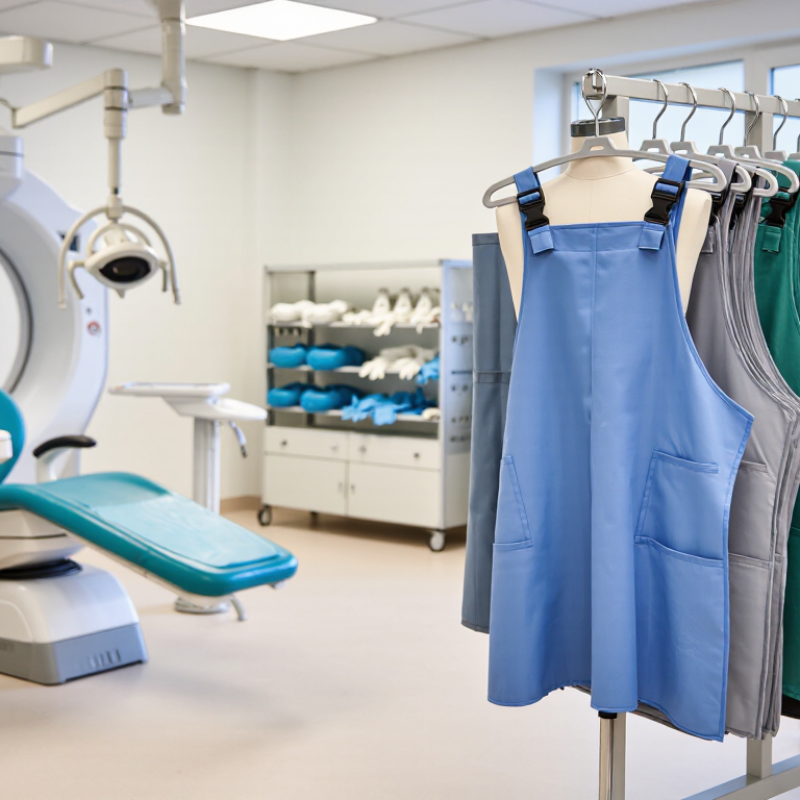
Table of Contents [Hide]
Defining Lead Apron Protection: 0.25–0.50 mm Pb Equivalence per IEC 61331-3
Best Lead Apron Manufacturer in China for Global Buyers
Defining lead apron protection starts with Pb equivalence, not apron weight. Under IEC 61331-3, common ratings include 0.25, 0.35, and 0.50 mm Pb equivalence. These values indicate shielding performance under defined test conditions. They do not describe ordinary fabric thickness.
A 0.50 mm rating is not automatically twice as useful as 0.25 mm. Protection depends on radiation energy, exposure direction, garment coverage, and correct fitting. In practical inspections, experienced buyers check the front panel, overlap areas, seams, and closures. Small gaps can reduce confidence during repeated clinical movement. Fit matters.
Reliable manufacturers should provide current test documentation, material specifications, size charts, and care instructions. Ask whether testing covers the finished garment, rather than only a raw sheet. Review batch identification and visual inspection records when possible. Hang aprons flat or on approved supports to reduce cracking. Never fold them casually.
Some purchasing decisions still focus too heavily on price. That is understandable, but incomplete. A lighter apron may improve comfort, while a higher rating may increase fatigue. The right choice needs workplace assessment and professional guidance. Even careful processes can miss hidden damage, so regular inspection remains necessary. Verify applicable requirements in the destination market before ordering.