- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
China Best Foil Roll Manufacturer for Global Buyers?
Choosing the China Best Foil Roll Manufacturer for Global Buyers requires more than comparing prices. A reliable supplier should demonstrate stable production, clear specifications, and practical export experience. The right partner understands thickness, width, alloy, temper, surface finish, and packaging requirements. These details affect sealing performance, forming quality, transport safety, and production efficiency. Small variations matter.
An experienced Foil Roll manufacturer usually provides traceable raw materials and documented quality procedures. Buyers should ask about chemical composition testing, thickness tolerance, tensile strength, pinhole inspection, and roll consistency. Factory audits can reveal useful details, including clean production areas, calibrated instruments, and organized storage. Samples are valuable, but repeated batches provide stronger evidence. One successful sample proves little.
Global buyers also need dependable communication. Technical drawings, inspection reports, packing photographs, and shipping documents should be accurate and easy to verify. A professional manufacturer can explain lead times, minimum order quantities, private labeling, and after-sales support without making vague promises. Relevant certifications may support credibility, but buyers should confirm their validity and scope. Certificates alone are not enough.
Real purchasing experience teaches a harder lesson. The lowest quotation may create higher costs later through delays, defects, or weak packaging. Even strong factories can make mistakes, so corrective actions and communication speed deserve attention. No supplier is perfect. That is why this guide examines manufacturing capability, product quality, compliance awareness, pricing, and long-term reliability. The goal is not to praise one company blindly, but to help buyers make a careful, evidence-based decision.
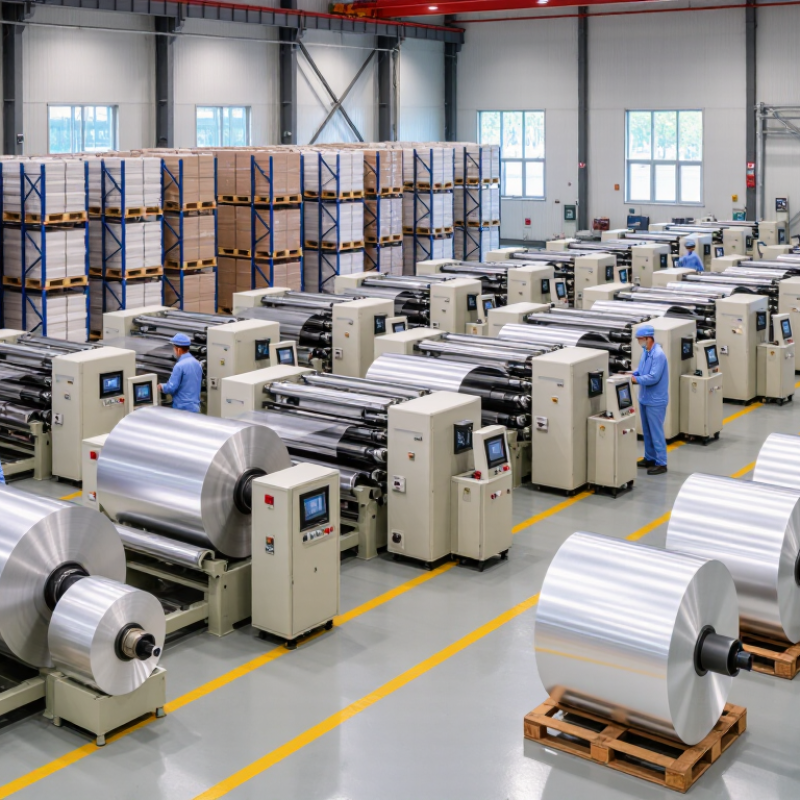
Table of Contents [Hide]
What Defines a Leading China Foil Roll Manufacturer
What Defines a Leading China Foil Roll Manufacturer
A leading China foil roll manufacturer is defined by process control, not attractive catalog images. Experienced buyers inspect alloy grades, thickness tolerance, roll width, and surface condition before discussing price. A reliable factory should provide clear technical data and production samples. Small details matter. A clean edge prevents feeding problems during later converting.
Manufacturing expertise appears in daily routines. Operators should monitor rolling pressure, annealing temperature, and tension throughout production. Quality teams can use calibrated gauges to check thickness at several points across each roll. They should also inspect pinholes, wrinkles, oil residue, and telescoping. Complete batch records make defects easier to trace. Photos alone are not enough.
Strong suppliers communicate honestly when a specification is difficult. They explain possible trade-offs between softness, strength, finish, and delivery speed. Packaging should protect rolls from moisture, crushing, and contamination during storage and transport. Export experience also includes accurate documents and responsive after-sales support. Yet no factory is flawless. Even a capable manufacturer may face an occasional deviation, so its correction process deserves close attention. A thoughtful buyer should request a sample, review inspection reports, and test the material in real equipment. That step may feel slow. It often prevents expensive surprises.
China Best Foil Roll Manufacturer for Global Buyers? - What Defines a Leading China Foil Roll Manufacturer
| Evaluation Dimension | Reliable Industry Benchmark | What a Leading Manufacturer Should Demonstrate | Recommended Buyer Verification |
|---|---|---|---|
| Material Range | Aluminium foil commonly supplied in alloy grades such as 1235, 8011, 8079 and 3003, depending on the end use. | Clear alloy certificates, controlled chemical composition and traceability from raw material to finished roll. | Request a mill test certificate and confirm the alloy designation against the product specification. |
| Thickness Capability | Commercial foil applications often use approximately 0.006–0.200 mm thickness, while household and food-packaging foil is usually in the thinner part of this range. | Stable rolling and annealing controls with documented thickness measurements across the full coil length. | Define nominal thickness, allowable tolerance and measurement method before placing an order. |
| Roll Width | Slit widths are selected according to the converting machine; jumbo coils are generally produced first and then slit to customer dimensions. | Modern slitting equipment, accurate width setup and clean, burr-free edges. | Confirm maximum jumbo width, finished width range, width tolerance and edge-condition requirements. |
| Dimensional Tolerance | Thickness, width, length and flatness tolerances should be agreed according to the applicable aluminium foil specification, such as EN 546 or ASTM B479. | Calibrated gauges, inspection records and a documented non-conformance process. | Include numerical tolerances and sampling frequency in the purchase specification. |
| Surface Quality | Surface should be free from significant oil stains, pinholes, wrinkles, dents, tears, foreign matter and excessive oxidation. | Visual inspection, pinhole testing where applicable, controlled rolling oil and protected handling. | Approve a retained reference sample and define acceptable defect limits. |
| Mechanical Properties | Temper conditions such as soft, half-hard and hard are selected according to forming, folding, sealing or converting requirements. | Consistent tensile strength, elongation and temper control supported by laboratory test records. | Specify tensile strength, elongation and temper instead of relying only on commercial terms such as “soft.” |
| Pinhole Control | Pinhole requirements vary significantly with thickness and application; pharmaceutical, food and barrier packaging normally require stricter control. | Defined inspection area, test method, acceptance limit and corrective-action records. | Ask for pinhole test results from the same production lot rather than a generic certificate. |
| Core and Winding | Paper, plastic or metal cores may be used; core inside diameter, coil outside diameter and winding direction must match the customer’s equipment. | Uniform tension, telescoping control, secure coil ends and accurately labelled roll identification. | Provide core size, maximum roll weight, outside diameter, winding direction and permitted joint length. |
| Food-Contact Suitability | Food-contact foil must comply with the regulations applicable in the destination market and with the intended food-contact conditions. | Appropriate declarations, raw-material traceability, hygiene controls and migration or compliance documentation when required. | State the destination market and request documentation covering the exact alloy, coating and application. |
| Quality Management | A mature quality system normally includes incoming inspection, process control, final inspection, calibration and corrective action. | A current quality-management certificate, internal inspection plans and batch-level records. | Verify certificate validity and audit the actual production site or request an independent inspection. |
| Production Traceability | Each finished roll should be traceable to its production date, alloy, heat or batch, processing route and inspection results. | Unique roll numbers, barcode or label systems and retained quality records. | Check whether the supplier can trace a delivered roll back to raw material and test data. |
| Packaging for Export | Export packaging should protect foil from moisture, impact, contamination and deformation during multimodal transport. | Moisture-resistant wrapping, suitable pallets or crates, edge protection and shock-resistant loading procedures. | Approve packaging drawings and confirm container loading, desiccant use and photograph records. |
| Lead-Time Reliability | Lead time depends on alloy, thickness, width, quantity, production schedule and port conditions; a fixed written schedule is more reliable than a general promise. | Production planning, capacity visibility and documented on-time delivery performance. | Request a production timeline covering order confirmation, material preparation, inspection and dispatch. |
| Minimum Order Quantity | MOQ varies by alloy, thickness, width, slit configuration and whether the order is a standard or custom specification. | Transparent pricing for standard sizes, custom sizes, trial orders and mixed-container shipments. | Obtain MOQ and surcharge rules in writing, including costs for custom cores, packaging and special testing. |
| Export Documentation | Common documents include commercial invoice, packing list, bill of lading, certificate of origin and quality or conformity documents when required. | Accurate documentation aligned with product labels, quantities, customs codes and destination-country requirements. | Review a sample document set before shipment and confirm responsibility for customs-related information. |
| Sustainability Performance | Aluminium is highly recyclable, but energy use, recycled content, process scrap recovery and packaging materials affect overall environmental performance. | Documented scrap-recycling practices, energy monitoring and measurable environmental objectives. | Request recycled-content information, environmental certificates and data on process scrap recovery. |
| Technical Support | Application-specific support is important for packaging, insulation, cable shielding, battery components and other converting processes. | Ability to recommend alloy, temper, thickness, surface condition and winding configuration based on the customer’s process. | Use a trial order and evaluate technical response time, sample consistency and corrective-action capability. |
Purchasing note: The benchmarks above are commonly used industry reference points. Final requirements should be confirmed in a signed technical specification because permissible tolerances, food-contact rules, testing methods and delivery conditions vary by application and destination market.