- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
China Best Fin Tube Manufacturers for Global Buyers
For global buyers, choosing among China’s fin tube manufacturers is not simply a matter of comparing prices. The right supplier must match the tube geometry, base material, fin type, operating temperature, and project specifications. A small difference in fin spacing can affect airflow, pressure drop, and cleaning access. Details matter.
Heat-transfer specialist Dr. Ramesh K. Shah’s work on compact heat exchangers supports a practical principle, paraphrased here: “Begin with the thermal duty, not the catalogue.” That distinction helps buyers ask sharper questions. Can the manufacturer provide material certificates, dimensional inspection records, and performance data for the proposed design? Are welding or brazing procedures documented? How are samples checked before production? These questions reveal more than a polished product page.
China’s supply base includes factories with different equipment, engineering depth, and quality systems. Some excel at standard copper-aluminum coils; others handle stainless steel, high-pressure service, or customized fin profiles. No supplier is perfect. A quote may look complete while leaving tolerances, test methods, or packaging unclear. Ask for those details in writing, then compare offers against the same specification. Request references where appropriate, and verify that stated certifications apply to the actual manufacturing site and product.
This guide examines how global buyers can assess Fin Tube manufacturers, compare technical capability, and reduce sourcing surprises. It cannot replace an application-specific engineering review. Still, careful questions at the start can prevent costly mismatches later. A little skepticism helps.
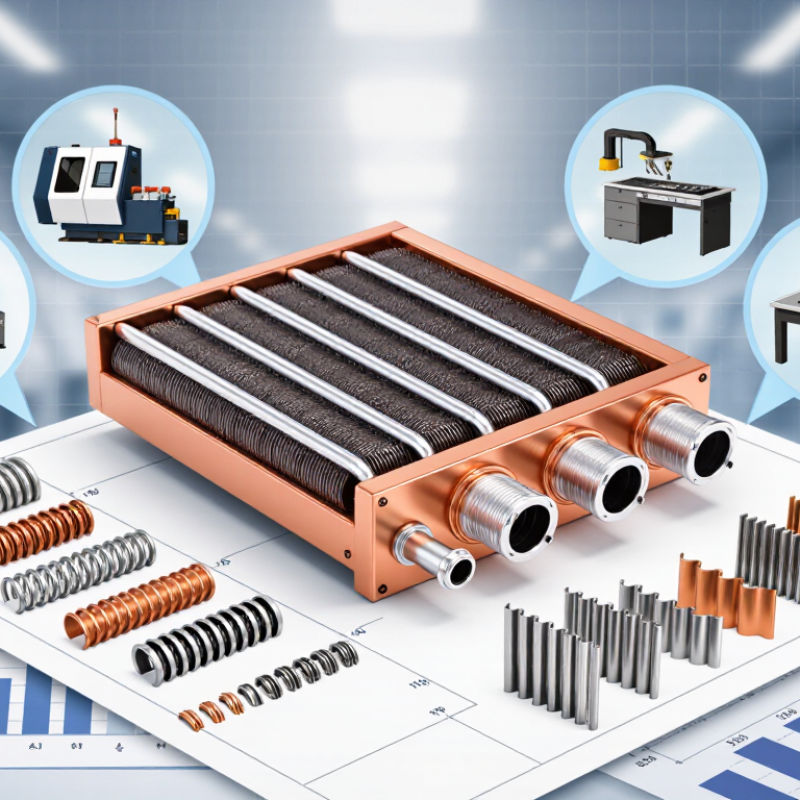
Table of Contents [Hide]
Fin Tubes Explained: Common 5–12 FPI Densities, Materials, and Applications
China Best Fin Tube Manufacturers for Global Buyers
Fin Tubes Explained: Common 5–12 FPI Densities, Materials, and Applications
FPI means fins per inch, a measure of fin spacing. Common designs range from 5 to 12 FPI. Around 5–6 FPI leaves wider passages for airflow and easier cleaning, which can suit dusty or oily environments. Higher densities, often 8–12 FPI, add surface area in a compact space. They may also increase airflow resistance and collect debris faster. It depends.
Fin materials are selected for heat transfer, corrosion exposure, weight, and cost. Aluminum fins are lightweight and common in HVAC and refrigeration coils. Copper can offer strong heat transfer, while stainless steel may suit demanding or corrosive conditions. The tube material matters too; matching fin and tube materials to the fluid and surroundings is essential. A denser fin is not automatically a better fin.
Tips: Share operating temperature, airflow, humidity, and expected contaminants when requesting a quotation. Confirm FPI, fin thickness, tube alloy, coating, and tolerances on the drawing. Ask how the unit can be cleaned and inspected. Datasheets can look complete yet miss practical details; check the actual spacing, not only the headline specification.