- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
2026 Best Abrasive Flap Disc for Global Buyers?
Choosing the 2026 best Abrasive Flap Disc requires more than comparing grit numbers or catalog prices. Global buyers need reliable performance across steel, stainless steel, aluminum, and coated surfaces. A disc that works smoothly in a European workshop may behave differently in a humid Asian factory. Material, machine speed, operator technique, and workload all matter.
This guide draws on practical grinding experience, supplier documentation, and measurable product criteria. We examine abrasive grain type, flap density, backing strength, disc diameter, grit range, and maximum operating speed. We also consider edge control, heat generation, vibration, and service life. Small details matter. Uneven flaps can leave visible marks. Excessive pressure may shorten disc life and damage the workpiece.
No single product is perfect.
A professional selection should match the application, not simply follow a popular brand. Buyers should verify test data, batch consistency, packaging quality, and supplier support before placing large orders. Independent performance checks can reveal differences hidden by attractive marketing claims. This is especially important for distributors managing multiple markets and safety expectations. The article also discusses how to compare total operating cost, not only the purchase price. A cheaper disc may require more replacements, create more rework, or reduce operator productivity. Some conclusions remain open to testing, because workshop conditions differ widely. Readers should treat recommendations as informed guidance, then confirm them with controlled trials, manufacturer specifications, and trained operators.
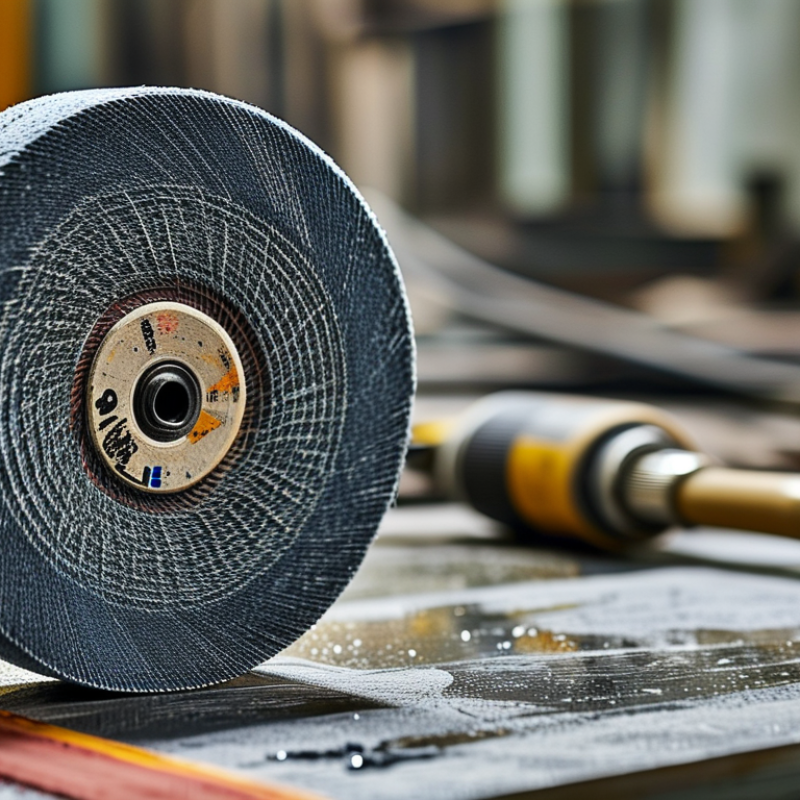
Table of Contents [Hide]
What Is an Abrasive Flap Disc and How Does It Work?
An abrasive flap disc is a wheel made from overlapping abrasive-cloth flaps. Each flap contains abrasive grains bonded to a flexible backing. The disc fits an angle grinder and spins at high speed. As the flaps contact metal, sharp grains cut away surface material. The backing supports the grains while allowing controlled flexibility.
The cutting action combines abrasion and slight flap movement. Worn grains break away, exposing newer cutting edges underneath. This helps the disc maintain performance during ordinary grinding work. Coarse grits remove welds, rust, and heavy scratches quickly. Fine grits create a smoother finish. The working angle also matters. A shallow angle usually suits blending, while a steeper angle increases material removal. Use moderate pressure. Excess force can overheat the workpiece and wear the flaps unevenly. I still sometimes press too hard on stubborn welds. That feels faster, but it usually shortens disc life.
For global buyers, selection should match the metal, finish, grinder, and workload. Check grit, diameter, bore size, flap material, and maximum RPM. The disc rating must meet or exceed the grinder’s speed. Inspect the disc before mounting. Cracked backing, loose flaps, or moisture damage require rejection. A disc may look usable while hiding weakened bonding. In workshop practice, clean contact and steady movement produce more consistent results than brute force. Safety glasses, face protection, gloves, and suitable work clothing remain essential during operation.