2026 Top Hot Melt Coating Machine Buying Guide

Hot Melt Coating Machine technology supports packaging, labels, hygiene products, medical materials, and industrial laminates. Buyers now need more than a listed speed or attractive price. They must examine coating width, adhesive viscosity, heating stability, web tension, and cleaning access. A machine may run at 150 meters per minute, yet poor temperature control can create visible streaks, weak bonds, and expensive material waste.

Grand View Research reported strong expansion in the global hot-melt adhesives market, supported by packaging, construction, and nonwoven applications. Its 2024–2030 analysis also identifies performance, sustainability, and production efficiency as important market drivers. Smithers’ report, The Future of Hot Melt Adhesives to 2028, highlights continuing demand for cleaner processing and reliable application systems. These findings matter because adhesive growth directly influences coating equipment requirements. However, market forecasts are not purchase guarantees.

Dr. James M. McKeen, an adhesive technology author, writes, “Hot melt adhesives are 100% solid materials that melt when heated and solidify when cooled.” That simple principle explains the machine’s central challenge: controlled heat. This guide compares tank capacity, slot-die accuracy, automatic viscosity management, PLC functions, energy use, and after-sales support. It also considers operator training and spare-part availability. No buying formula is perfect. A low-cost machine can become expensive when filters clog weekly or service takes months. Buyers should test their actual adhesive, substrate, coating weight, and production speed before signing. Small trials reveal uncomfortable truths. They also protect long-term investment.

2026 Top Hot Melt Coating Machine Buying Guide

Hot Melt Coating Machine Basics: Systems, Materials, and 5–150 g/m² Coat Weights

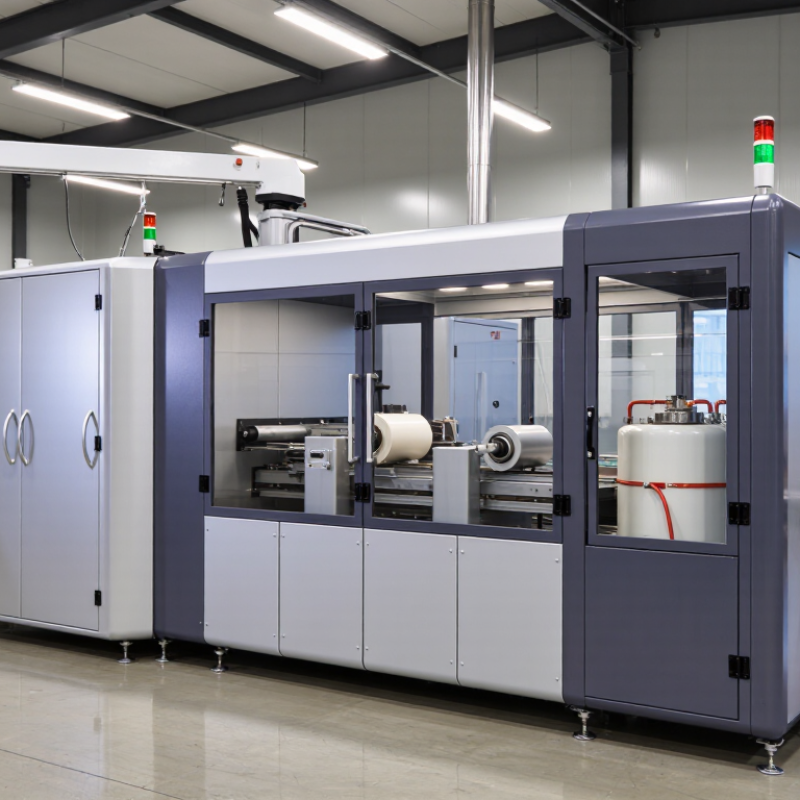
A hot melt coating machine applies adhesive without water or solvent, using controlled heat and pressure. Its core system includes a heated tank, metering pump, heated hose, coating head, and web-handling unit. A slot die supports accurate thin layers, while a roll coater can suit broader process conditions. Stable temperature control matters because small thermal changes can alter viscosity and coating weight.

Materials must match the substrate and final application. EVA often offers practical bonding and processing, while polyamide supports higher heat resistance. TPU may provide flexibility, but it can require tighter drying and storage control. Reactive polyurethane needs careful moisture management and compatible equipment. Always check the adhesive supplier’s technical data, especially melt viscosity, open time, and processing temperature.

Coat weight selection usually ranges from 5 to 150 g/m². Low weights demand precise pumping, clean surfaces, and steady web tension. Higher weights require stronger pumping capacity and effective heat removal after coating. A gravimetric check can reveal whether the target weight is real. Do not trust machine settings alone. A common mistake is choosing speed before confirming coating uniformity. In production trials, I would measure across the web, inspect edge build-up, and record temperature changes every shift. Some results may still look acceptable while bond strength slowly declines. That deserves further testing.

2026 Top Hot Melt Coating Machine Buying Guide - Hot Melt Coating Machine Basics: Systems, Materials, and 5–150 g/m² Coat Weights

A practical comparison of hot melt coating machine systems, compatible materials, operating ranges, and purchasing criteria. Actual performance depends on adhesive chemistry, substrate, coating width, line speed, and process conditions.

Category Parameter Typical Data or Range Practical Application Key Buying Check
Machine Basics Coating technology Slot-die Roll coating Spray coating Contact coating Continuous coating of films, foils, papers, nonwovens, textiles, labels, tapes, and laminates. Match the coating head to the required coat-weight accuracy, substrate surface, and operating speed.
Machine Basics Typical coating width Approximately 300–2,000 mm for many converting lines; custom widths may be smaller or larger. Narrow-web label and tape production through wide-web film, paper, and nonwoven processing. Specify usable coating width, web width, edge trim, and future width requirements separately.
Machine Basics Line-speed range Approximately 10–300 m/min for many hot melt coating applications; the usable range varies by adhesive and substrate. Low-speed specialty coating, medium-speed converting, and high-speed adhesive coating. Verify speed at the target coat weight, not only the machine's maximum mechanical speed.
Coating System Slot-die system Pre-metered coating with a controlled die gap and pump-fed adhesive delivery. Uniform full-width coating, pressure-sensitive adhesive, hygiene materials, medical products, and laminating webs. Check die-lip design, shim or gap adjustment, pump stability, and cleaning access.
Coating System Roll coating system Metered coating using one or more heated rolls; suitable for contact transfer and selected gravure-style processes. Tapes, release liners, textiles, papers, and applications requiring robust web contact. Evaluate roll surface finish, runout, nip control, pressure adjustment, and adhesive release behavior.
Coating System Spray coating system Atomized or filament-style hot melt application for patterned, intermittent, or breathable coating. Nonwovens, hygiene products, construction materials, filters, and moisture-permeable laminates. Confirm pattern resolution, nozzle maintenance, overspray control, and ventilation requirements.
Coating System Adhesive melting and delivery Melt tank or heated hopper, heated hose, heated pump, and heated coating head. Maintains adhesive in a molten state from loading through application. Check independent temperature zones, insulation, melt-level sensing, filtration, and hose flexibility.
Coating System Temperature control Common operating temperatures are approximately 120–190°C, depending on adhesive chemistry and supplier guidance. Stable viscosity and consistent flow during melting, pumping, and coating. Use multi-zone control, calibrated sensors, over-temperature protection, and recipe management.
Materials EVA hot melt adhesive Ethylene-vinyl acetate based; commonly selected for general-purpose bonding and packaging applications. Paper, board, selected films, packaging components, and general assembly. Confirm compatibility with the substrate, required open time, bond strength, and thermal resistance.
Materials SBC hot melt adhesive Styrene block copolymer based; available in formulations for pressure-sensitive and elastic bonding. Labels, tapes, elastic attachments, hygiene products, and flexible laminates. Check viscosity stability, tack, shear resistance, elasticity, and sensitivity to heat or oxidation.
Materials Polyolefin hot melt adhesive Polyolefin-based formulations with low odor and good moisture resistance in suitable grades. Packaging, nonwoven laminating, film bonding, and applications requiring clean processing. Verify adhesion to low-surface-energy films and the required processing temperature.
Materials Polyamide hot melt adhesive Higher-performance hot melt chemistry with comparatively strong heat and chemical resistance. Technical textiles, electrical components, automotive-related parts, and demanding industrial bonding. Confirm melt temperature, moisture sensitivity, substrate compatibility, and equipment heat capacity.
Materials Reactive polyurethane hot melt Moisture-reactive hot melt that develops additional strength after exposure to atmospheric moisture. Durable laminating and assembly applications requiring high final bond performance. Require sealed material handling, moisture control, suitable hose and head design, and correct purging procedures.
Coat Weight 5–15 g/m² Light coat-weight range. Light laminating, breathable constructions, selected labels, and low-add-on adhesive layers. Prioritize precise metering, low-flow stability, clean die lips, and accurate web tension control.
Coat Weight 15–40 g/m² Low-to-medium coat-weight range. Pressure-sensitive tapes, labels, flexible laminates, and many nonwoven bonding processes. Compare pump turndown, cross-web uniformity, coating-head adjustment, and line-speed capability.
Coat Weight 40–80 g/m² Medium coat-weight range. Stronger laminating bonds, technical textiles, protective materials, and heavier adhesive layers. Check melt capacity, heated-zone recovery, filtration, and substrate cooling or support requirements.
Coat Weight 80–150 g/m² High coat-weight range. Heavy-duty laminates, construction products, thick nonwovens, and high-add-on coating applications. Confirm pump capacity, thermal power, die-flow distribution, web support, and safe operator access.
Metering Coat-weight control Calculated from adhesive mass flow and coated area; commonly monitored by pump output, line speed, and coating width. Maintains target adhesive consumption and helps control bond performance. Request gravimetric or laboratory verification procedures and cross-web uniformity data.
Web Handling Tension control Closed-loop tension control using load cells, dancer systems, or drive synchronization. Reduces wrinkles, stretching, lateral movement, and coating defects on flexible substrates. Check tension range, sensor placement, automatic splicing compatibility, and substrate-specific recipes.
Quality Typical process checks Coat weight, cross-web uniformity, bond strength, peel, tack, visual defects, and web alignment. Confirms that the coating meets functional and appearance requirements. Ensure the machine can integrate inspection, sampling, data logging, and alarm functions.
Safety Operator protection Guarding, emergency stops, thermal cut-outs, pressure relief, insulation, and hot-surface warnings. Protects operators from heated adhesive, moving rolls, pressurized lines, and electrical hazards. Review risk assessment, guarding access, lockout procedures, exhaust provisions, and training requirements.
Maintenance Cleaning and changeover Purge cycles, removable filters, accessible die or nozzles, heated flushing, and controlled adhesive drain paths. Reduces downtime and helps prevent carbonized adhesive, blocked nozzles, and cross-contamination. Ask for estimated cleaning time, spare-part requirements, approved purge materials, and maintenance access.
Energy Heating and operating efficiency Energy demand depends on melt throughput, temperature setpoints, line speed, insulation, ambient conditions, and startup frequency. Affects operating cost and adhesive thermal history. Compare insulated zones, standby modes, startup time, heat recovery, and actual energy data at the target process.
Purchase Planning Recommended specification package Substrate details, adhesive type, coat-weight range, coating width, line speed, temperature, roll diameter, and quality targets. Creates a clear technical basis for machine selection and acceptance testing. Require a documented process trial using the intended adhesive and production substrate before final approval.

Important: The listed ranges are general industry planning values rather than guaranteed machine specifications. Final selection should be validated through an application trial with the intended adhesive, substrate, coat weight, coating width, and production speed.

Key Buying Specifications: 10–100 m/min Speed and 300–2,000 mm Web Widths

A hot melt coating machine should match your actual production range, not an impressive maximum speed. For many converters, 10–100 m/min offers a practical balance between coating stability and changeover time. At lower speeds, adhesive streaks and uneven edges become easier to detect. At higher speeds, viscosity control, web tension, and cooling require closer attention. A 300–2,000 mm web width range supports both narrow trials and wider commercial rolls.

Market demand supports this flexibility. Grand View Research valued the global flexible packaging market at approximately USD 261.07 billion in 2022 and forecast a 4.2% compound annual growth rate through 2030. Smithers’ flexible packaging research also identifies lightweight structures and recyclable designs as continuing development priorities. These trends increase the need for accurate coat-weight control, stable temperature zones, and fast width adjustments. Small details matter.

When comparing machines, request test data at your target adhesive, substrate, speed, and coating weight. Ask for measured results, not only brochure limits. A machine rated at 100 m/min may deliver poorer coating uniformity near its maximum. That assumption can fail. Check temperature accuracy, unwind tension, edge control, cleaning access, and operator safety systems. Leave room for process learning. Real production rarely behaves like a perfect laboratory trial.

2026 Top Hot Melt Coating Machine Buying Guide

Typical web-width planning ranges across the 10–100 m/min coating-speed envelope. Use these values as a specification reference when comparing machine configurations; final requirements depend on coating material, substrate, and process stability.

The chart covers the stated buying range of 10–100 m/min and 300–2,000 mm web widths. Higher-speed lines generally require wider and more robust web-handling systems, while narrower webs can be suitable for lower-throughput or specialty coating applications.

Heating and Application Performance: 80–180°C Operating Temperature Ranges

2026 Top Hot Melt Coating Machine Buying Guide

Heating and Application Performance: 80–180°C Operating Temperature Ranges

A reliable hot melt coating machine should control heat, not merely reach a high temperature. The 80–180°C range covers many coating materials and production needs. Lower settings near 80–110°C can reduce thermal stress on sensitive films and substrates. Higher settings near 140–180°C may support faster flow and smoother coverage. However, excessive heat can darken adhesive, increase viscosity changes, and damage delicate liners. Application temperature, hose temperature, and die temperature must remain balanced. Small differences matter.

The 2024 MarketsandMarkets Hot Melt Adhesives Market report projects continued market growth through 2028, driven by packaging, hygiene, and assembly applications. This expansion increases demand for stable coating control and lower material waste. Buyers should examine heating-zone accuracy, warm-up time, insulation, and temperature recovery after line stoppages. A displayed setpoint is not proof of uniform heat. Test the coating across the full web width. Record surface temperature, coat weight, and viscosity during trials. Real production conditions often expose problems that laboratory tests miss.

Tips: Start trials at the lowest workable temperature. Increase heat gradually. Check the actual adhesive temperature, not only the controller reading. Ask suppliers for thermal mapping data and maintenance records. Do not overlook cleaning access. It can decide whether performance remains stable after several shifts. Some specifications look impressive, but the evidence may be thin. Review them carefully.

Control and Quality Standards: ±2% Coat-Weight Accuracy and Online Monitoring

2026 Top Hot Melt Coating Machine Buying Guide

A ±2% coat-weight tolerance should be a purchasing requirement, not a sales promise. It means a 20 g/m² target should remain between 19.6 and 20.4 g/m².

That narrow window demands stable temperature, pump pressure, web tension, and die alignment. In production trials, a warm-up drift of only 3°C can visibly change coating coverage. It is easy to blame the die. Sometimes, the measurement system is wrong.

Online monitoring brings control closer to the coating point. A reliable system should measure coat weight continuously, display trends, and trigger alarms before defects spread across a roll. The 2024 Deloitte Smart Manufacturing and Operations Survey found that 92% of manufacturers view smart manufacturing as important to future competitiveness. Smithers’ flexible packaging market analysis also identifies automation and process control as continuing investment priorities. These findings support digital monitoring, but they do not replace operator judgment.

Tips: Ask suppliers for recorded data, not screenshots. Check sensor calibration with a traceable reference. Compare readings across startup, steady running, and shutdown. Review the machine’s response time after a ±2% deviation. Also test imperfect conditions, such as low viscosity or uneven substrate tension. A machine that performs only in ideal conditions may become expensive very quickly.

Total Cost Evaluation: Energy Use, Maintenance, Safety, and Return on Investment

2026 Top Hot Melt Coating Machine Buying Guide

Total cost begins with energy, not the purchase price. The IEA’s Energy Efficiency 2023 report identifies industry as roughly 37% of global final energy consumption. A hot melt coater may consume power through heating zones, pumps, chillers, and compressed air. Request measured kWh per production hour, not only rated motor power. Compare this figure at startup, normal speed, and idle. Small leaks matter. The U.S. Department of Energy reports that poorly maintained compressed-air systems can waste 20–30% of compressor output. That waste can quietly increase coating costs.

Maintenance changes the investment calculation. Ask for heater replacement intervals, pump service requirements, filter costs, and technician access time. Record unplanned stops in your model. A two-hour shutdown may cost more than a replacement part. Safety also has a financial value. Include guarding, emergency stops, thermal protection, ventilation, and operator training. A machine that reduces exposure to hot adhesive may lower risk, but verify the design against applicable workplace standards. Do not accept vague compliance claims.

Tips: Build a five-year ownership sheet. Add electricity, consumables, labor, service visits, downtime, and disposal costs. Calculate payback using conservative output assumptions. Test a sample run before purchasing. Payback can disappoint. Energy-saving settings may reduce speed or coating uniformity. Review that trade-off with production records, not sales estimates. The final decision should compare cost per saleable square meter, supported by utility bills, maintenance logs, and documented safety checks.