- High-Performance Doors
-
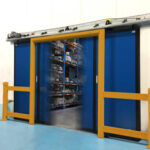
- Applications
-
-
-
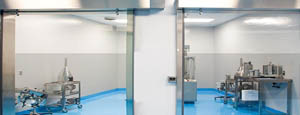
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
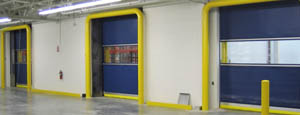
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
2026 Best Drilling Rig API 6A Check Valve Manufacturers
Choosing among the 2026 best Drilling Rig API 6A Check Valve manufacturers requires more than comparing catalog prices. These valves protect pressure-control systems during drilling, testing, and well servicing. A dependable model should match the required working pressure, bore size, temperature range, and fluid conditions. Small details matter. A damaged hinge, weak seal, or unclear material record can create serious operational concerns.
This guide examines manufacturers through practical and technical criteria. These include API 6A compliance, pressure testing, body materials, sealing performance, manufacturing capacity, and traceability. Reliable suppliers should provide clear inspection records, heat-treatment information, test certificates, and consistent quality-control procedures. Their valves should also suit sour-service requirements when specified by the operating environment. Experienced buyers often review machining accuracy, coating quality, spare-part availability, and technical support before approval.
A strong reputation helps, but it does not replace evidence. Factory audits, independent inspection, and project references can reveal differences hidden behind similar product descriptions. No shortlist is perfect. Some manufacturers publish limited testing details, while others offer excellent documentation but slower delivery. That trade-off deserves attention. The best choice depends on verified performance, realistic service conditions, and long-term support. This article presents a careful comparison to help drilling contractors, equipment integrators, and procurement teams make a more confident decision. Safety remains central. Reliability is demonstrated in records, testing, and field behavior—not in promotional language alone.
Table of Contents [Hide]
What an API 6A Check Valve Is in Drilling Rig Systems
2026 Best Drilling Rig API 6A Check Valve Manufacturers
What an API 6A Check Valve Is in Drilling Rig Systems
An API 6A check valve is a pressure-control component that permits fluid to move in one direction. It helps prevent reverse flow through wellhead, choke, kill, and other high-pressure systems. During drilling operations, pressure can change quickly. A reliable check valve helps protect pumps, manifolds, and connected equipment from sudden backflow.
Its internal disc or piston responds to fluid pressure without constant operator control. When flow moves correctly, the valve opens. When flow reverses, it closes against the seat. Selection requires more than matching pipe size. Engineers should verify pressure rating, temperature range, bore size, end connections, material class, and sour-service requirements. API 6A compliance should also include documented inspection, testing, and traceability.
Tips: Check the valve’s nameplate against the purchase specification. Review body and seat test records. Inspect sealing surfaces for scratches, corrosion, or trapped debris before installation. Small particles can cause serious leakage.
In practical field work, installation quality often decides performance. Incorrect flow direction, poor alignment, or damaged seals can defeat a well-designed valve. I have seen specifications focus heavily on pressure while overlooking maintenance access. That is a weakness worth correcting. No valve selection is perfect. Conditions change, and operating data may be incomplete. A careful review should include expected pressure surges, fluid characteristics, inspection intervals, and replacement plans. Reliable manufacturers should provide clear technical documents, consistent quality control, and support that remains useful after delivery.