- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
2026 Best Seamless Carbon Steel Pipe Suppliers?
Choosing the 2026 best Seamless Carbon Steel Pipe Supplier requires more than comparing prices. It requires evidence, field experience, and disciplined technical review. A reliable supplier should explain its steel grades, manufacturing route, heat-treatment records, dimensional tolerances, and inspection procedures. Certificates alone are not enough.
Quality expert W. Edwards Deming offered a useful warning: “Quality comes not from inspection, but from the improvement of the production process.” His principle fits seamless pipe procurement closely. Buyers should examine how billets are heated, pierced, rolled, treated, tested, and traceably marked. A strong supplier can connect one pipe to its material certificate, test report, and production batch.
Look closely.
This guide evaluates suppliers through practical details. It considers API and ASTM familiarity, ultrasonic testing, hydrostatic testing, surface condition, delivery consistency, and technical support. It also examines whether the supplier understands actual service conditions, including pressure, temperature, corrosion exposure, and installation limits.
The best supplier is not always the largest exporter. A smaller mill may offer better communication and tighter inspection control. However, that assumption can fail without independent verification. Procurement teams should request recent project references, sample documentation, and clear responses to nonconformance questions.
Some claims deserve skepticism. “Premium quality” means little without measurable acceptance criteria. A dependable Seamless Carbon Steel Pipe Supplier welcomes technical questions and identifies limitations honestly. That behavior matters when pipes arrive at a construction site, where a missed tolerance or unclear grade can delay welding, testing, and commissioning.
This article compares leading suppliers for 2026 using practical, evidence-based criteria. It aims to support careful decisions, not quick rankings.
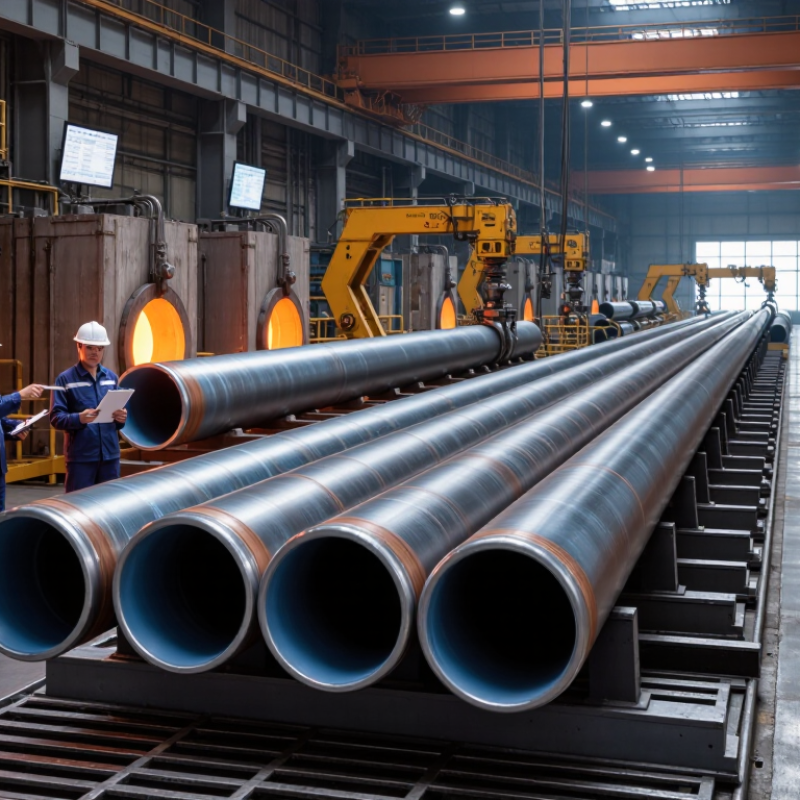
Table of Contents [Hide]
What Are Seamless Carbon Steel Pipes?
A seamless carbon steel pipe is formed without a welded seam. Manufacturers heat a solid steel billet, pierce it, then roll it into a hollow tube. This structure can provide consistent strength around the circumference. It is not automatically stronger in every application. Grade, wall thickness, heat treatment, and production quality still matter. Carbon steel mainly contains iron and carbon, with limited alloying elements. It offers good mechanical strength, machinability, and cost control. It also transfers heat efficiently in many industrial systems. However, moisture and aggressive chemicals can cause corrosion. That weakness is easy to underestimate. Surface protection or corrosion-resistant design may be necessary.
In practical use, these pipes carry oil, gas, water, steam, and process fluids. They appear in boilers, pressure lines, structural supports, and energy equipment. Engineers select them by pressure, temperature, fluid chemistry, diameter, and required service life. A pipe that suits a low-pressure water line may fail in a hot, pressurized system. Small details matter. Check dimensional tolerances, test records, heat numbers, and applicable standards before purchasing. Visual inspection can reveal dents, scale, or poor end preparation. Yet appearance alone proves little. Independent testing may verify chemical composition, tensile strength, hardness, and hydrostatic performance. In my view, supplier evaluation should include traceability and consistent documentation, not price alone. That judgment deserves review when project conditions change. Buyers should compare actual service requirements with the pipe specification.
2026 Best Seamless Carbon Steel Pipe Suppliers? - What Are Seamless Carbon Steel Pipes?
| Data Dimension | Specification or Property | Verified Technical Data | Why It Matters When Selecting a Supplier |
|---|---|---|---|
| Product definition | Seamless carbon steel pipe | A tubular steel product manufactured without a longitudinal welded seam. It is generally produced by piercing a heated billet and reducing or sizing the hollow shell. | The absence of a welded seam can be advantageous for high-pressure, high-temperature, and cyclic-service applications, subject to the applicable standard and design conditions. |
| Typical chemical composition | Carbon steel chemistry | Primarily iron and carbon, with controlled amounts of manganese, silicon, phosphorus, and sulfur. Exact limits depend on the selected specification and grade. | A supplier should provide a heat-specific mill test certificate showing chemical analysis and compliance with the ordered standard. |
| Common specification | ASTM A106 Grade B | Seamless carbon steel pipe for high-temperature service. Minimum tensile strength: 415 MPa; minimum yield strength: 240 MPa. | Suitable for many refinery, power-generation, process, and high-temperature piping systems when the design code permits it. |
| Common specification | ASTM A53 Grade B, Type S | Type S designates seamless manufacture. Minimum tensile strength: 415 MPa; minimum yield strength: 240 MPa. | Often used for mechanical and pressure applications, water, air, steam, and general industrial piping, subject to project requirements. |
| Common specification | API 5L Grade B, PSL 1 | Line pipe grade with minimum tensile strength of 415 MPa and minimum yield strength of 245 MPa for Grade B. | Used for transportation of oil, gas, and other fluids. The purchaser must specify the required product specification level, testing, and delivery condition. |
| Low-temperature service | ASTM A333 Grade 6 | Seamless or welded carbon steel pipe for low-temperature service. Minimum tensile strength: 415 MPa; minimum yield strength: 240 MPa. Grade 6 is commonly specified with impact testing at −45 °C. | Useful for cold-service piping where impact toughness is required, provided the complete purchase specification confirms the test temperature and acceptance criteria. |
| European pressure-piping grade | EN 10216-2 P265GH | Non-alloy steel tube for pressure purposes. Typical specified minimum yield strength is 265 MPa; tensile strength is generally 410–570 MPa, depending on product conditions and dimensions. | Provides a European-standard option for pressure equipment and elevated-temperature service when the applicable design rules accept the material. |
| Outside diameter and wall thickness | Dimensional control | Pipe dimensions are normally ordered by nominal pipe size, outside diameter, and wall thickness or schedule. ASME B36.10M covers many dimensions for wrought steel pipe. | Confirm actual outside-diameter, wall-thickness, length, end-preparation, and dimensional-tolerance requirements before placing an order. |
| Wall-thickness options | Schedule 10 to XXS and custom thicknesses | Standard schedules include 10, 20, 30, 40, 60, 80, 100, 120, 140, and 160; XS and XXS are also used. Availability depends on size, standard, and production route. | The correct wall thickness must be calculated from pressure, temperature, corrosion allowance, external loads, and the governing design code. |
| Length supply | Random and fixed lengths | Common commercial descriptions include single random length, double random length, and fixed length. Exact ranges and tolerances are controlled by the applicable standard or purchase order. | Length accuracy affects installation time, cutting waste, welding quantities, and total project cost. |
| Manufacturing process | Hot-finished or cold-drawn | Hot-finished pipe is formed and sized at elevated temperature. Cold-drawn pipe is further processed at room temperature for tighter dimensional control and improved surface finish. | Select the process according to dimensional tolerance, surface finish, mechanical properties, and application requirements. |
| Inspection documentation | Mill test certificate and inspection report | A complete document package may include heat number, chemical analysis, tensile test, yield test, elongation, hardness where required, hydrostatic or nondestructive test results, and dimensional inspection. | Traceable documentation helps verify conformity, supports audits, and reduces the risk of receiving material that does not meet the purchase specification. |
| Pressure testing | Hydrostatic or approved nondestructive testing | Testing requirements vary by standard. Hydrostatic testing verifies pressure integrity; electromagnetic or ultrasonic examination may be required as an alternative or supplement. | The supplier should state the test method, test pressure or acceptance criteria, calibration status, and whether results are included in the inspection dossier. |
| End preparation | Plain, beveled, threaded, or grooved ends | Plain ends are commonly used for smaller sizes or mechanical connections; beveled ends support butt welding; threaded and grooved ends are used where specified by the piping system. | Correct end preparation improves fit-up and prevents additional machining, rework, or installation delays. |
| Primary applications | Industrial fluid and structural service | Common uses include process piping, oil and gas transportation, boilers, heat exchangers, water systems, mechanical components, structural columns, and pressure equipment. | The best supplier is determined by compliance with the required standard, grade, dimensions, testing, documentation, delivery capability, and service conditions—not by price alone. |
Note: Technical values shown are minimum or typical specification requirements and should be verified against the latest edition of the applicable standard and the project design code before procurement.