- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources
2026 Best Greenhouse Pipe Types for Global Buyers
For global buyers, choosing the right Greenhouse Pipe affects structural safety, crop protection, and long-term operating costs. In 2026, suppliers offer galvanized steel, aluminum, PVC, and HDPE options for different greenhouse environments. Each material behaves differently under wind, snow, humidity, and repeated temperature changes. The strongest option is not always the most suitable.
Small details matter. A galvanized steel pipe may provide excellent load-bearing strength, but poor coating quality can invite rust around cut edges and welded joints. Aluminum resists corrosion and reduces installation weight, yet it may require stronger connectors in high-wind regions. PVC is economical for smaller structures, although prolonged sunlight can make lower-grade products brittle. HDPE offers useful flexibility, but its performance depends heavily on wall thickness and connection design.
Experienced buyers should examine pipe diameter, thickness, zinc coating, tensile strength, and supplier testing records. Ask for clear specifications, factory quality controls, and shipment documentation. Local climate data also matters more than a global product ranking. A pipe suitable for a mild coastal nursery may fail under heavy snow or desert heat. That assumption is often wrong.
This guide compares leading Greenhouse Pipe types for international purchasing decisions. It considers durability, installation, maintenance, transport, and total lifecycle value. Some cost comparisons remain imperfect because freight rates and regional labor prices change quickly. Still, careful technical review can reduce expensive mistakes and support safer, more productive greenhouse construction.
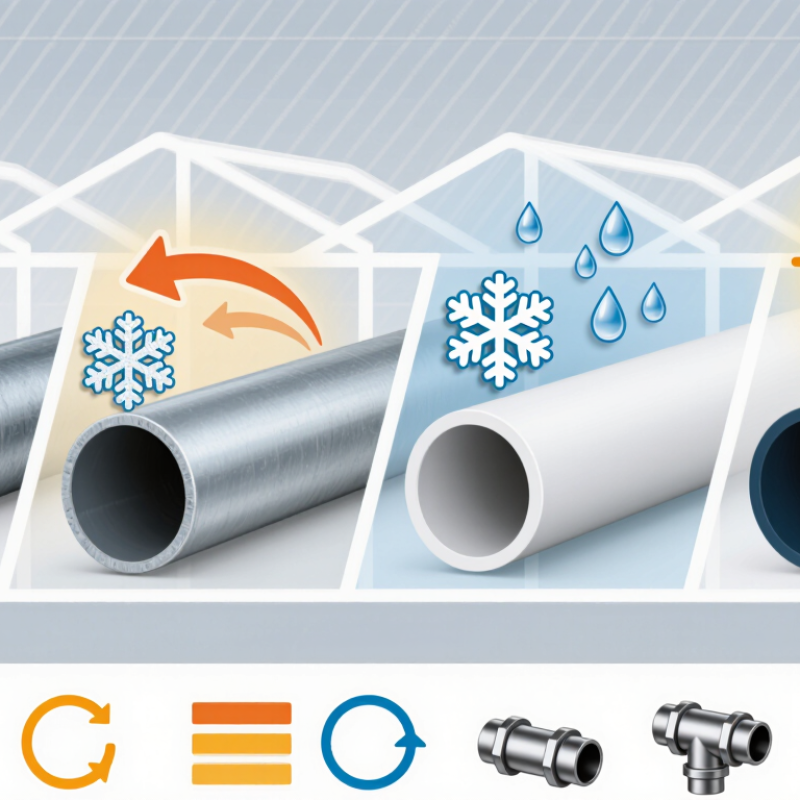
Table of Contents [Hide]
What Are Greenhouse Pipes and Why Do They Matter?
Greenhouse pipes form the hidden framework that keeps a growing space stable. They support the roof, side curtains, irrigation lines, heating tubes, and ventilation equipment. Without correctly selected pipes, even a well-designed greenhouse can sag, leak, or shift under strong wind.
Common choices include galvanized steel, aluminum, and PVC. Galvanized steel offers high strength for large structures and heavy snow loads. Aluminum resists rust and reduces structural weight. PVC is practical for water delivery and temporary systems, but it needs careful protection from sunlight and heat. Pipe diameter, wall thickness, coating quality, and connection design all affect service life.
Climate should guide every purchase. Coastal air can accelerate corrosion, while dry regions may expose pipes to intense ultraviolet radiation. A buyer should check load calculations, local building requirements, and available replacement fittings. Inspecting a cut section can reveal thin walls or uneven coatings. Small details matter.
Do not choose by price alone.
In practical installation, poorly aligned joints often create more trouble than weak pipes. I have also seen specifications look impressive while ignoring transport damage and repair access. That is a useful warning. A reliable pipe system needs suitable materials, accurate measurements, and realistic maintenance planning. Even the best pipe can fail when installers force mismatched connectors or leave standing water inside the line.